


Single-stage In-line High Shear Mixer
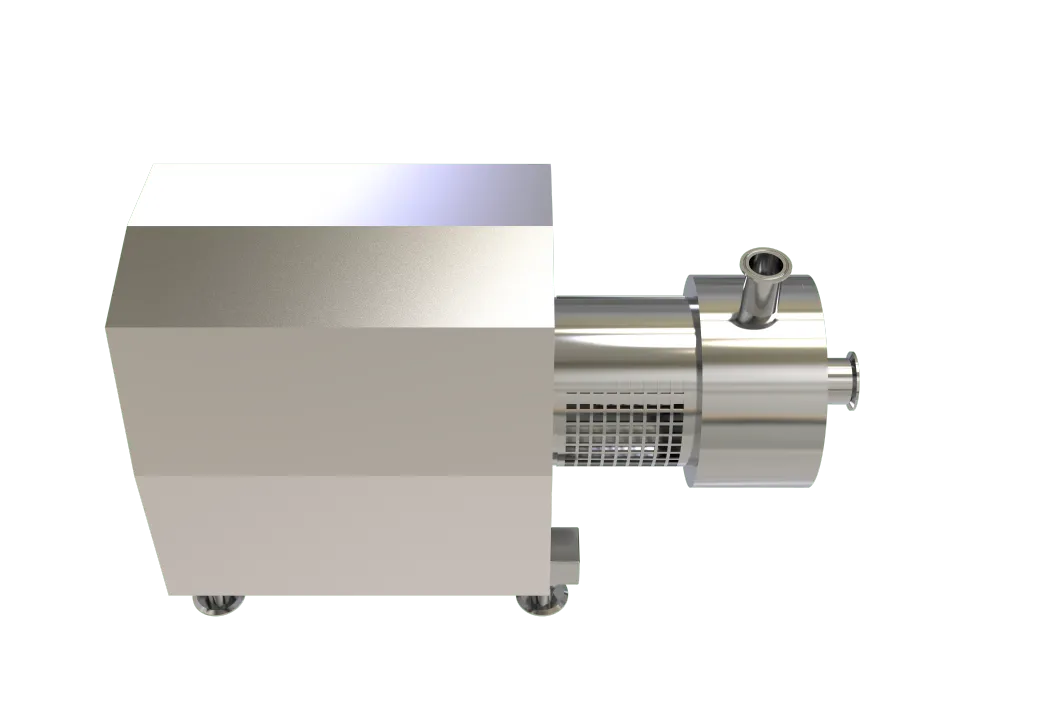
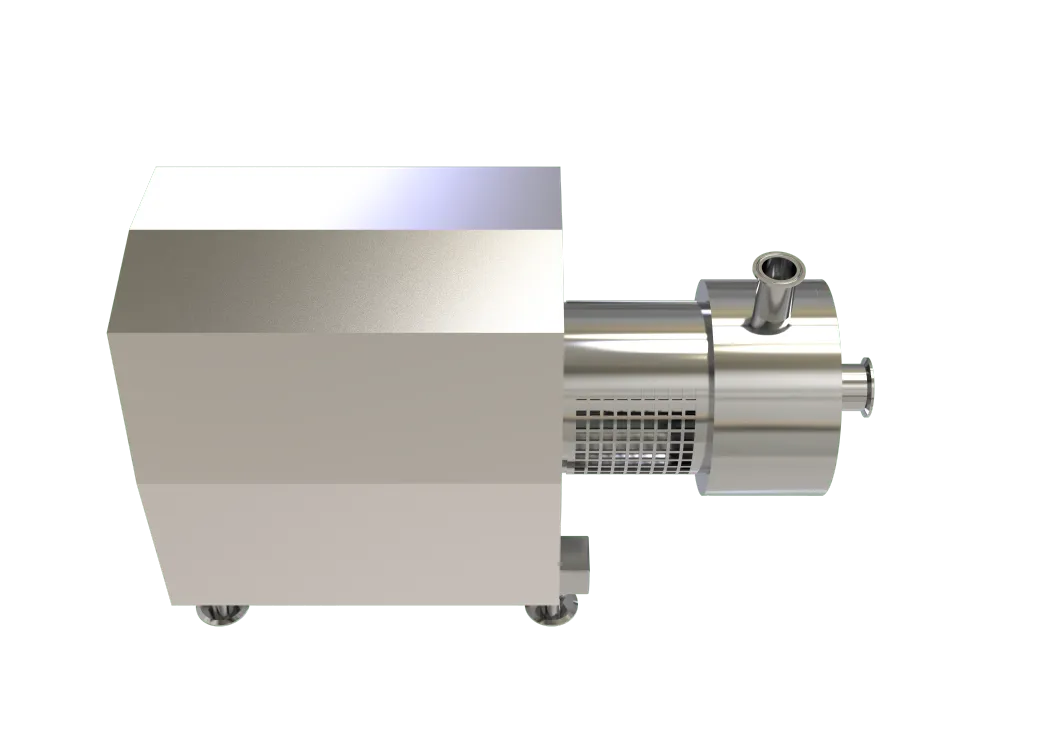
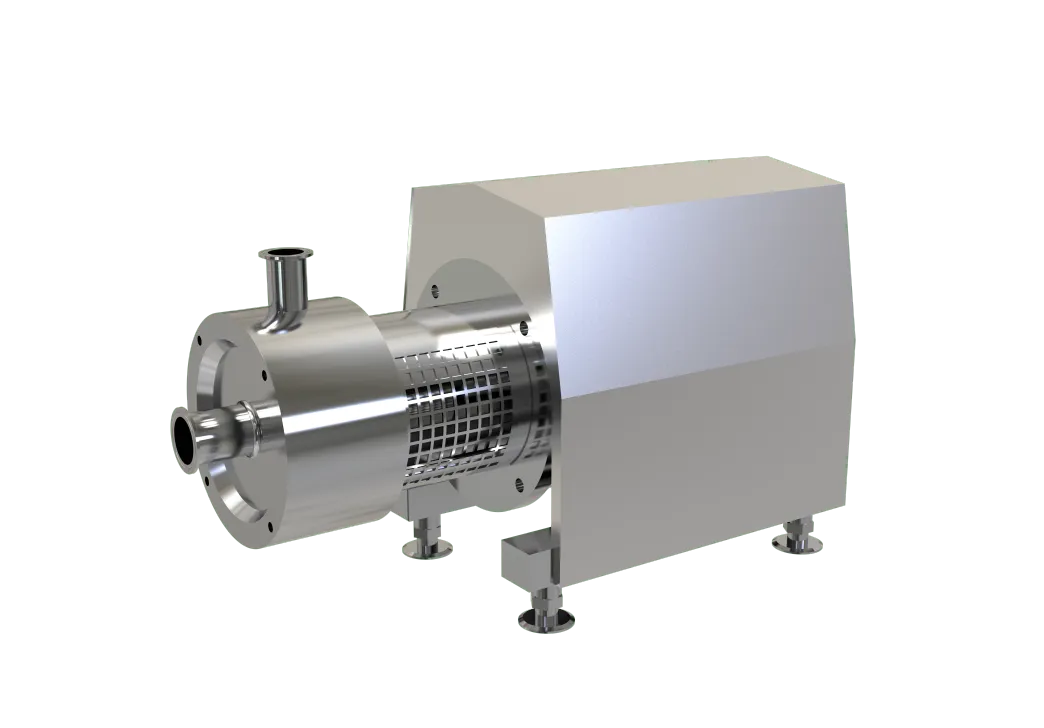
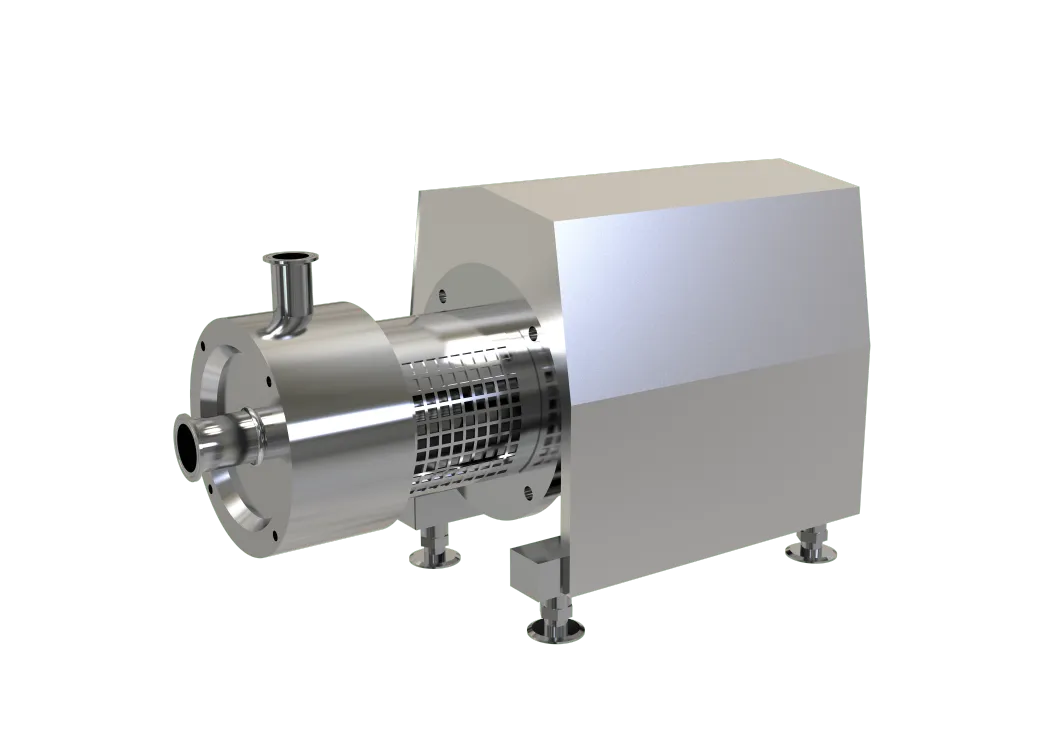
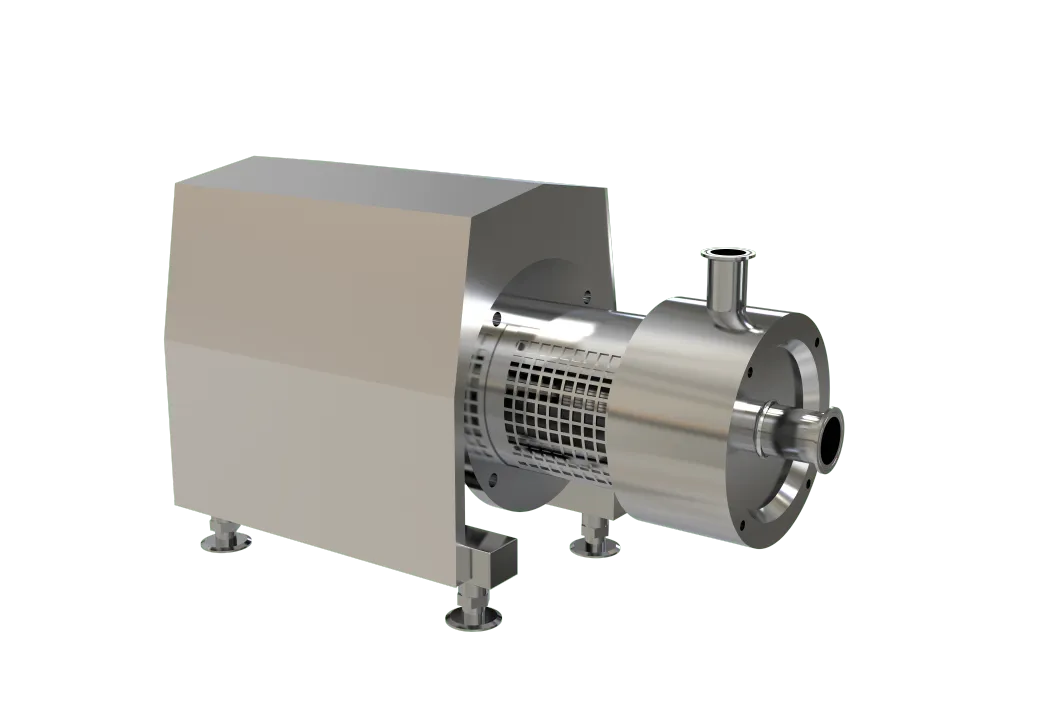
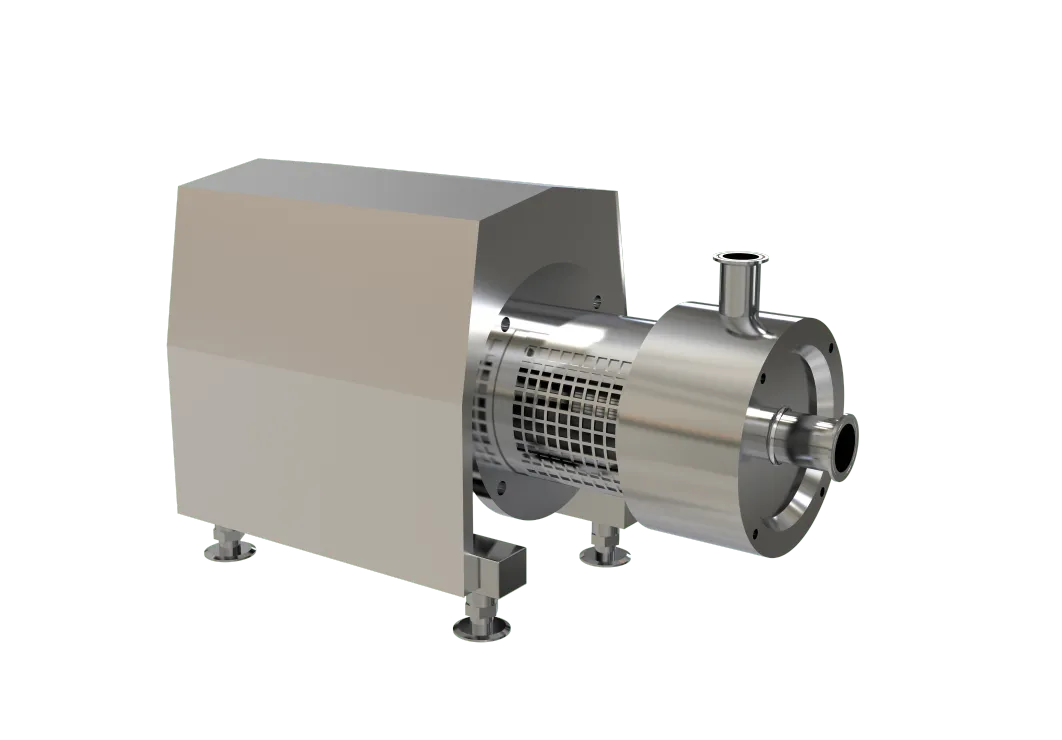
In modern process engineering, achieving homogeneous multi-phase fluid mixtures requires high-efficiency processing equipment that minimizes energy consumption while maximizing continuous throughput. The single-stage in-line high shear mixer, commonly referred to as an emulsification pump, represents a foundational technology within fine chemical, biopharmaceutical, food, and petrochemical manufacturing lines. By replacing traditional batch processing equipment like sand mills, ball mills, or colloid mills, this continuous inline device significantly slashes operational runtimes and ensures uniform product batches. This technical guide outlines the internal mechanics, optional configurations, and specific system integration parameters governing this critical fluid engineering component.
Core Mechanics and Working Principles
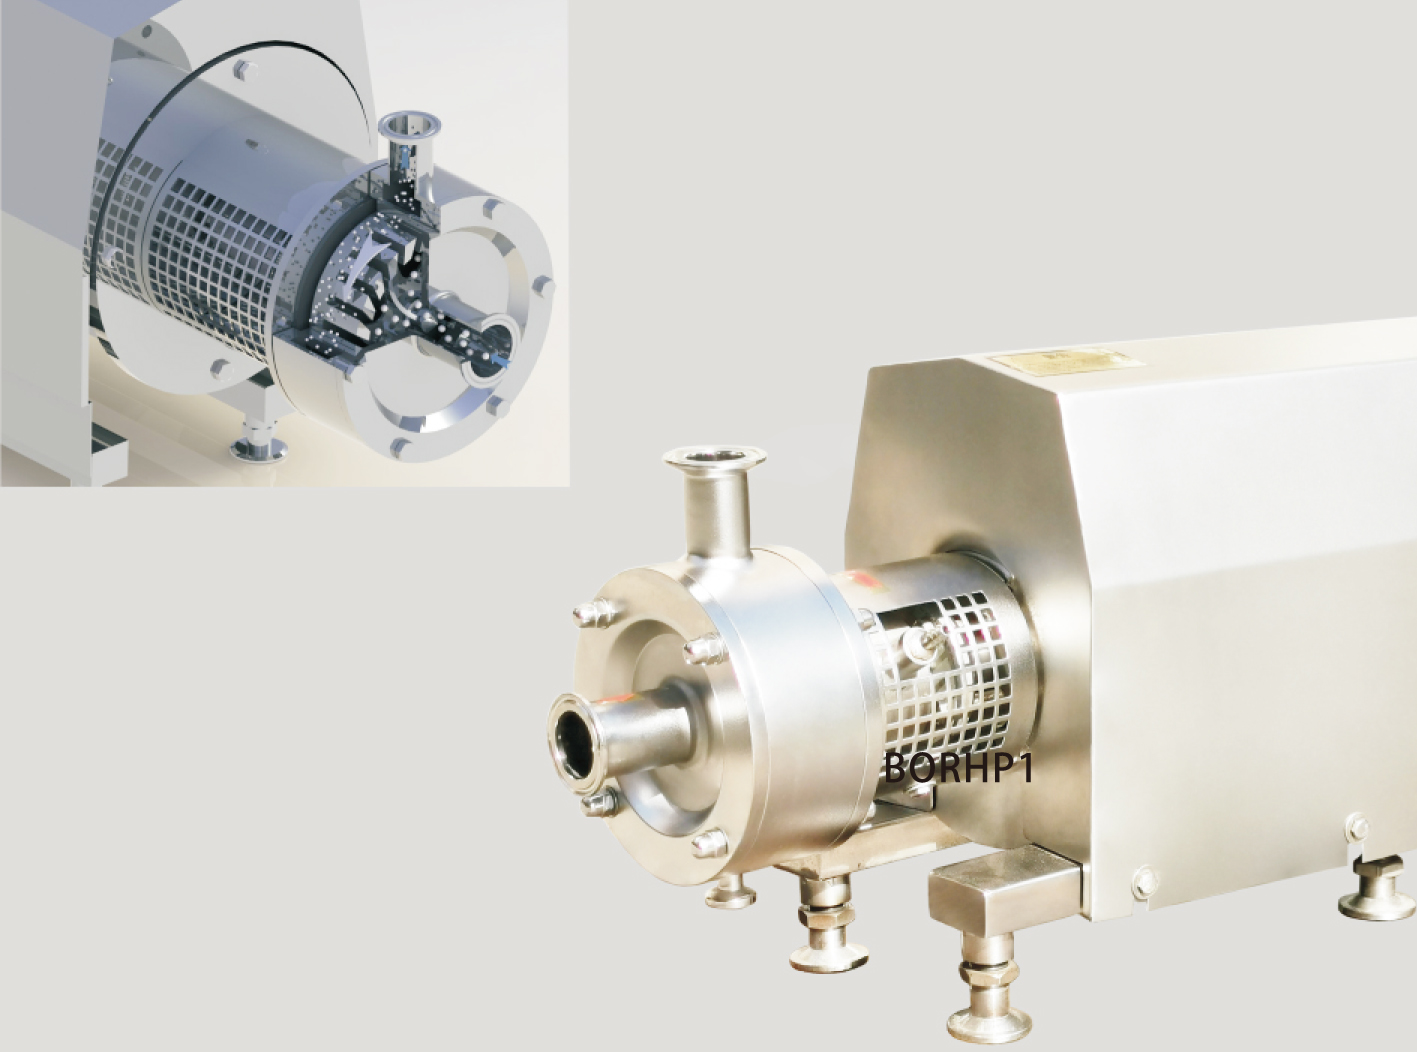
The operational framework of a single-stage in-line high shear mixer is driven by a precision-engineered rotor and stator assembly contained within a single mixing chamber. When the system is energized, the centrally mounted rotor rotates at linear speeds typically reaching twenty to forty meters per second, driven by a high-velocity motor running at two thousand nine hundred revolutions per minute. This high-speed rotation generates massive centrifugal forces immediately surrounding the internal fluid inlet channel, acting as a localized fluid pump that draws raw unmixed multi-phase materials into the center of the working head.
As fluid enters the rotor, it is accelerated radially outward at high velocities, experiencing intense kinetic energy transfer. The primary mechanical action occurs when the material reaches the microscopic gap between the outer edge of the rotor blades and the inner walls of the stationary stator. This gap, typically measuring less than one millimeter, creates an environment of extreme hydraulic shear, localized cavitation, and violent turbulent flows.
The fluid experiences multi-directional impact forces as it is forced through the precision-machined slots or perforations of the stator ring. Large solid agglomerates or coarse liquid droplets are instantly shattered by the combined forces of rapid fluid layer friction, high-frequency pressure pulsations, and localized high-velocity impact. After exiting the stator perimeter, the fluid is discharged from the chamber through the outlet nozzle. Because the physical volume of the internal chamber is tightly restricted, one hundred percent of the process fluid must pass directly through the active shear zone, eliminating short-circuiting or bypass paths. For processes requiring ultra-fine particle sizes or narrow droplet distributions, the outlet piping can be redirected back into the source vessel, establishing a closed-loop recirculation process loop that continuously refines the emulsion over time.
Core Performance Advantages and Operating Parameters
Integrating an in-line high shear emulsification pump into a continuous production line yields significant mechanical and financial advantages over old-fashioned batch tank mixing setups. One of the main technical advantages is the high volume throughput capacity combined with a localized low-head pumping effect. The unique hydraulic flow profiles inside the shear head allow the mixer to handle short-distance fluid transport and fluid elevation, which often reduces the need for independent auxiliary feed pumps within the immediate process pipework.
Furthermore, the mechanical precision of the high-speed rotor-stator architecture yields an exceptionally narrow particle and droplet size distribution profile. By applying uniform mechanical forces to all fluid elements, the single-stage mixer eliminates product quality variances between production batches, a common issue in traditional tank agitation systems. The smooth, balanced rotation of the dynamically balanced rotor ensures that the entire mixing pump operates with low acoustic noise levels and minimal structural vibration. This mechanical stability reduces physical wear on internal bearings and dynamic seals, lengthening overall maintenance intervals.
From an energy efficiency standpoint, processing raw materials on a continuous, single-pass or inline recirculation loop requires significantly less total power consumption compared to maintaining long-term agitation in a large product vessel. The concentrated application of mechanical shear directly onto the fluid stream ensures that electrical energy is converted into kinetic dispersion forces, optimizing the overall thermal and power profiles of the processing facility.
Material Engineering and Configurable Options
Industrial procurement demands high levels of equipment customization to ensure compatibility with aggressive chemical formulations, strict sanitation mandates, and explosive atmosphere classifications. Single-stage inline high shear mixers feature highly modular architectures that allow system engineers to specify exact material pairings across several mechanical subsystems:
- Chamber and Metallurgy Materials: The standard wetted parts are manufactured from high-grade austenitic stainless steel. Operators can select grade 304 stainless steel for non-corrosive industrial liquids or low-carbon grade 316L stainless steel for food-grade, cosmetics, and biopharmaceutical applications where chemical resistance and corrosion prevention are paramount.
- Elastomers and Static Seals: To prevent external leakage and survive chemical flush cycles, static seals are specified based on chemical compatibility. Options include Ethylene Propylene Diene Monomer for standard hot water and steam environments, Silicone for generic pharmaceutical fluids, or Fluororubber for aggressive chemical solvents, hydrocarbons, and high-temperature oils.
- Mechanical Shaft Sealing: The dynamic shaft seal separating the process chamber from the drive motor represents a critical configuration point. Single mechanical seals suffice for non-hazardous, self-lubricating fluids. However, double mechanical seals are mandatory for toxic, abrasive, or volatile materials. The double seal arrangement allows for an external barrier fluid flush system to cool the seal faces and contain any microscopic process migration. Seal face material pairings include carbon-to-silicon carbide, carbon-to-tungsten carbide, or tungsten carbide-to-tungsten carbide for highly abrasive slurry processing.
- Process Pipe Connections: For seamless system integration, the inlet and outlet ports can be machined with quick-connect tri-clamp fittings, SMS union threads, DIN union couplings, or heavy-duty industrial flanges to match pre-existing plant piping.
- Electrical Motors and Surface Finishes: Drive motors are available in standard enclosed configurations or explosion-proof variations certified for hazardous areas containing flammable vapors. Motor power levels are typically mapped to either standard two-pole configurations or four-pole designs designated with a specific suffix to indicate high-torque output profiles. Finally, external and internal metal surfaces can be customized with a sandblasted finish or a highly reflective mirror-polished finish to prevent bacterial adhesion and streamline manual cleaning operations.
System Selection Metrics and Operational Integration
Selecting the correct model from a range of high shear emulsification pumps requires careful analysis of flow rates, motor power ratings, and pipeline sizing. The primary operational matrix relies on aligning the targeted volumetric flow rate with the physical dimensions of the inlet and outlet process lines. Standard commercial line-up parameters are defined across a spectrum of industrial scale capacities:
For pilot plants or small-scale batch production lines, units operating with a flow rate of 3 to 5 cubic meters per hour utilize a compact motor rating between 2.2 and 4 kilowatts. These small-capacity configurations feature an inlet diameter of DN40 paired with a slightly restricted outlet diameter of DN32 to maintain optimal internal chamber pressure and velocity, operating with an exit pressure threshold between 0.05 and 0.08 Megapascals.
As production scales up to intermediate capacities, such as 10, 15, or 20 cubic meters per hour, the power requirements rise to 7.5, 11, and 18.5 kilowatts, respectively. These intermediate systems require a larger inlet piping footprint, scaling from DN50 to DN65, with corresponding outlet dimensions of DN40 to DN50, generating active discharge pressures up to 0.20 Megapascals.
At the highest tier of continuous industrial manufacturing, high-throughput pumps handle flow volumes of 30, 50, and 80 cubic meters per hour. These large-scale systems demand high-power electric motors rated at 22, 37, and 55 kilowatts to rotate the large-diameter heavy rotor assemblies against fluid resistance. The process connections for these heavy-duty units are expanded to DN80, DN100, and DN125 on the inlet side, and DN65, DN80, and DN100 on the outlet side. They deliver significant fluid energy, generating output pressures ranging from 0.25 up to 0.35 Megapascals while maintaining a stable shaft rotation velocity of 2900 revolutions per minute. By precisely matching these physical dimensions and power metrics to the viscosity and density profile of the target liquid, engineering teams can implement an optimized, long-lasting emulsification line that ensures steady product quality.

Description
In modern process engineering, achieving homogeneous multi-phase fluid mixtures requires high-efficiency processing equipment that minimizes energy consumption while maximizing continuous throughput. The single-stage in-line high shear mixer, commonly referred to as an emulsification pump, represents a foundational technology within fine chemical, biopharmaceutical, food, and petrochemical manufacturing lines. By replacing traditional batch processing equipment like sand mills, ball mills, or colloid mills, this continuous inline device significantly slashes operational runtimes and ensures uniform product batches. This technical guide outlines the internal mechanics, optional configurations, and specific system integration parameters governing this critical fluid engineering component.
Core Mechanics and Working Principles
The operational framework of a single-stage in-line high shear mixer is driven by a precision-engineered rotor and stator assembly contained within a single mixing chamber. When the system is energized, the centrally mounted rotor rotates at linear speeds typically reaching twenty to forty meters per second, driven by a high-velocity motor running at two thousand nine hundred revolutions per minute. This high-speed rotation generates massive centrifugal forces immediately surrounding the internal fluid inlet channel, acting as a localized fluid pump that draws raw unmixed multi-phase materials into the center of the working head.
As fluid enters the rotor, it is accelerated radially outward at high velocities, experiencing intense kinetic energy transfer. The primary mechanical action occurs when the material reaches the microscopic gap between the outer edge of the rotor blades and the inner walls of the stationary stator. This gap, typically measuring less than one millimeter, creates an environment of extreme hydraulic shear, localized cavitation, and violent turbulent flows.
The fluid experiences multi-directional impact forces as it is forced through the precision-machined slots or perforations of the stator ring. Large solid agglomerates or coarse liquid droplets are instantly shattered by the combined forces of rapid fluid layer friction, high-frequency pressure pulsations, and localized high-velocity impact. After exiting the stator perimeter, the fluid is discharged from the chamber through the outlet nozzle. Because the physical volume of the internal chamber is tightly restricted, one hundred percent of the process fluid must pass directly through the active shear zone, eliminating short-circuiting or bypass paths. For processes requiring ultra-fine particle sizes or narrow droplet distributions, the outlet piping can be redirected back into the source vessel, establishing a closed-loop recirculation process loop that continuously refines the emulsion over time.
Core Performance Advantages and Operating Parameters
Integrating an in-line high shear emulsification pump into a continuous production line yields significant mechanical and financial advantages over old-fashioned batch tank mixing setups. One of the main technical advantages is the high volume throughput capacity combined with a localized low-head pumping effect. The unique hydraulic flow profiles inside the shear head allow the mixer to handle short-distance fluid transport and fluid elevation, which often reduces the need for independent auxiliary feed pumps within the immediate process pipework.
Furthermore, the mechanical precision of the high-speed rotor-stator architecture yields an exceptionally narrow particle and droplet size distribution profile. By applying uniform mechanical forces to all fluid elements, the single-stage mixer eliminates product quality variances between production batches, a common issue in traditional tank agitation systems. The smooth, balanced rotation of the dynamically balanced rotor ensures that the entire mixing pump operates with low acoustic noise levels and minimal structural vibration. This mechanical stability reduces physical wear on internal bearings and dynamic seals, lengthening overall maintenance intervals.
From an energy efficiency standpoint, processing raw materials on a continuous, single-pass or inline recirculation loop requires significantly less total power consumption compared to maintaining long-term agitation in a large product vessel. The concentrated application of mechanical shear directly onto the fluid stream ensures that electrical energy is converted into kinetic dispersion forces, optimizing the overall thermal and power profiles of the processing facility.
Material Engineering and Configurable Options
Industrial procurement demands high levels of equipment customization to ensure compatibility with aggressive chemical formulations, strict sanitation mandates, and explosive atmosphere classifications. Single-stage inline high shear mixers feature highly modular architectures that allow system engineers to specify exact material pairings across several mechanical subsystems:
- Chamber and Metallurgy Materials: The standard wetted parts are manufactured from high-grade austenitic stainless steel. Operators can select grade 304 stainless steel for non-corrosive industrial liquids or low-carbon grade 316L stainless steel for food-grade, cosmetics, and biopharmaceutical applications where chemical resistance and corrosion prevention are paramount.
- Elastomers and Static Seals: To prevent external leakage and survive chemical flush cycles, static seals are specified based on chemical compatibility. Options include Ethylene Propylene Diene Monomer for standard hot water and steam environments, Silicone for generic pharmaceutical fluids, or Fluororubber for aggressive chemical solvents, hydrocarbons, and high-temperature oils.
- Mechanical Shaft Sealing: The dynamic shaft seal separating the process chamber from the drive motor represents a critical configuration point. Single mechanical seals suffice for non-hazardous, self-lubricating fluids. However, double mechanical seals are mandatory for toxic, abrasive, or volatile materials. The double seal arrangement allows for an external barrier fluid flush system to cool the seal faces and contain any microscopic process migration. Seal face material pairings include carbon-to-silicon carbide, carbon-to-tungsten carbide, or tungsten carbide-to-tungsten carbide for highly abrasive slurry processing.
- Process Pipe Connections: For seamless system integration, the inlet and outlet ports can be machined with quick-connect tri-clamp fittings, SMS union threads, DIN union couplings, or heavy-duty industrial flanges to match pre-existing plant piping.
- Electrical Motors and Surface Finishes: Drive motors are available in standard enclosed configurations or explosion-proof variations certified for hazardous areas containing flammable vapors. Motor power levels are typically mapped to either standard two-pole configurations or four-pole designs designated with a specific suffix to indicate high-torque output profiles. Finally, external and internal metal surfaces can be customized with a sandblasted finish or a highly reflective mirror-polished finish to prevent bacterial adhesion and streamline manual cleaning operations.
System Selection Metrics and Operational Integration
Selecting the correct model from a range of high shear emulsification pumps requires careful analysis of flow rates, motor power ratings, and pipeline sizing. The primary operational matrix relies on aligning the targeted volumetric flow rate with the physical dimensions of the inlet and outlet process lines. Standard commercial line-up parameters are defined across a spectrum of industrial scale capacities:
For pilot plants or small-scale batch production lines, units operating with a flow rate of 3 to 5 cubic meters per hour utilize a compact motor rating between 2.2 and 4 kilowatts. These small-capacity configurations feature an inlet diameter of DN40 paired with a slightly restricted outlet diameter of DN32 to maintain optimal internal chamber pressure and velocity, operating with an exit pressure threshold between 0.05 and 0.08 Megapascals.
As production scales up to intermediate capacities, such as 10, 15, or 20 cubic meters per hour, the power requirements rise to 7.5, 11, and 18.5 kilowatts, respectively. These intermediate systems require a larger inlet piping footprint, scaling from DN50 to DN65, with corresponding outlet dimensions of DN40 to DN50, generating active discharge pressures up to 0.20 Megapascals.
At the highest tier of continuous industrial manufacturing, high-throughput pumps handle flow volumes of 30, 50, and 80 cubic meters per hour. These large-scale systems demand high-power electric motors rated at 22, 37, and 55 kilowatts to rotate the large-diameter heavy rotor assemblies against fluid resistance. The process connections for these heavy-duty units are expanded to DN80, DN100, and DN125 on the inlet side, and DN65, DN80, and DN100 on the outlet side. They deliver significant fluid energy, generating output pressures ranging from 0.25 up to 0.35 Megapascals while maintaining a stable shaft rotation velocity of 2900 revolutions per minute. By precisely matching these physical dimensions and power metrics to the viscosity and density profile of the target liquid, engineering teams can implement an optimized, long-lasting emulsification line that ensures steady product quality.
Application


Specifications
Advantage Comparison


GET IN TOUCH NOW


